Heavy Duty Industrial Floating Ball Valve
The Heavy Duty Industrial Floating Ball Valve is a cornerstone component in modern industrial fluid control systems, engineered to handle extreme operating conditions while delivering reliable, leak-tight performance. Unlike trunnion-mounted alternatives, its floating ball design leverages fluid pressure to create a secure seal, making it ideal for high-pressure, high-temperature applications across diverse sectors. At its core, the valve features a spherical ball with a through-hole (bore) that aligns with the pipeline to allow flow or rotates 90 degrees to block it. The ball is not fixed to the stem or body; instead, it “floats” between two sealing seats. When fluid flows, upstream pressure pushes the ball against the downstream seat, forming a tight seal that prevents leakage—even under fluctuating pressure conditions. This self-sealing mechanism eliminates the need for additional sealing forces in many cases, simplifying design and enhancing reliability. Constructed from robust materials to withstand harsh environments, the valve’s body is typically cast from carbon steel, stainless steel (304/316), or alloy steels (e.g., Chrome-Moly) for corrosion and high-temperature resistance. The ball is often made of hardened stainless steel or alloyed with Stellite to boost wear resistance, critical for handling abrasive fluids. Seats are application-specific: PTFE or polymer seats for low-temperature, non-abrasive media, and metal seats (Stellite, Inconel) for high-temperature (up to 550°C) or abrasive flows. The stem includes a blowout-proof feature to prevent accidental ejection under pressure, using stainless steel or alloy materials for durability. Key specifications include pressure ratings from ANSI Class 150 to 2500, temperature ranges from cryogenic (-196°C) to extreme heat, and end connections like flanged (ANSI/ASME), threaded (NPT/BSP), or welded (socket/butt weld). Full-bore options minimize flow restriction, while reduced-bore variants offer cost savings. Many models comply with API 607 (fire-safe design) to maintain sealing integrity during fires and API 6D (pipeline valves) for pipeline use. Large valves often integrate gear operators to reduce torque, ensuring ease of use for high-pressure systems. These valves are indispensable in oil and gas (upstream exploration, midstream pipelines, downstream refineries), chemical processing (corrosive acids/solvents), power generation (steam/cooling water), water treatment (high-pressure desalination), and mining (slurries). For example, in refineries, they control crude oil and refined products under high pressure, while in chemical plants, they manage corrosive fluids safely. The primary benefits include exceptional sealing reliability, long service life, versatility across fluids/conditions, and low maintenance (few moving parts, easy inspection). Fire-safe and blowout-proof designs enhance safety, reducing leak risks and environmental hazards. Their compact form allows installation in tight spaces, making them a preferred choice for industrial engineers. In summary, the Heavy Duty Industrial Floating Ball Valve is a critical asset for industries needing robust fluid control. Its innovative design, durable construction, and adherence to strict standards ensure it meets the demands of even the most challenging environments, driving efficient, safe, and cost-effective operations.
Products
Category:
Ball Valve
-
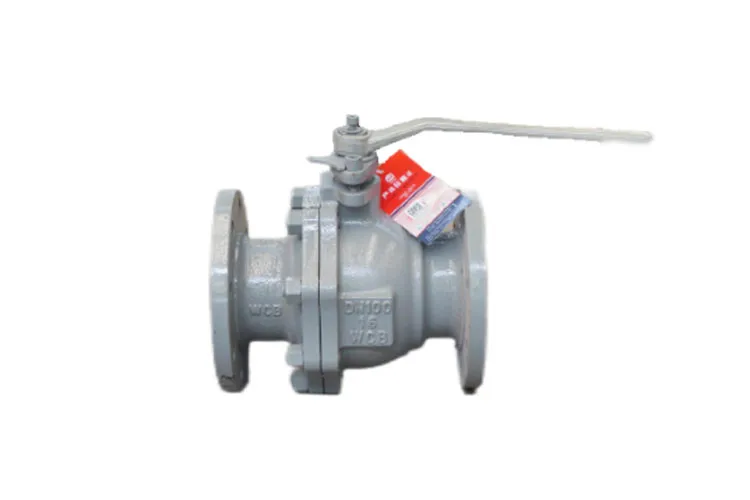
Heavy Duty Industrial Applications Floating Ball Valve
Category: Ball ValveBrowse number:Number:Release time: 2026-10-18 11:55:26The Heavy Duty Industrial Applications Floating Ball Valve is engineered for reliable performance in demanding industrial environments. Designed to handle high-pressure and high-temperature media, this valve features a robust floating ball design that ensures precise flow control and tight sealing. Manufactured from durable corrosion-resistant materials, it withstands abrasive and corrosive fluids, extending service life and minimizing maintenance. Ideal for chemical, petrochemical, oil & gas, and water treatment pipelines, this valve provides efficient operation, leak-free performance, and long-term reliability. Upgrade your industrial pipeline system with the Floating Ball Valve for Heavy Duty Industrial Applications for enhanced safety and operational efficiency.
News
Category:
-
[Industry News]Floating Ball Physics Experiments for Beginners
2026-04-11 07:58:28 -
[Industry News]Trunnion Mounted Ball Valve Design Standards
2026-03-12 12:16:07
Case
Category:
No search results found!
Video
Category:
No search results found!
Download
Category:
No search results found!
Job
Category:
No search results found!
Featured Products
No search results found!


 Phone