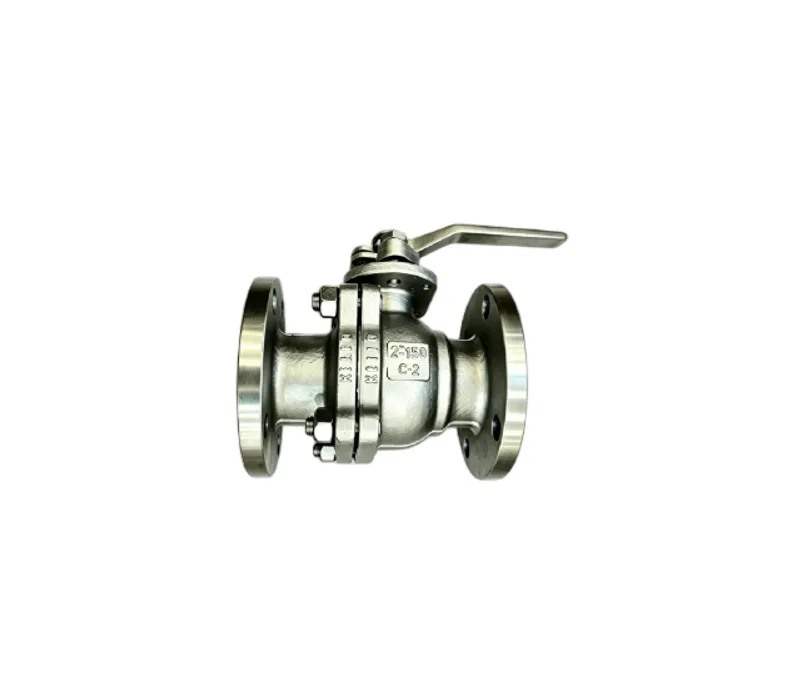
The main function of a ball valve is to cut off or open the fluid passage in a pipeline. Its working principle is that a driving device applies a certain torque to the upper end of the valve stem, which is transmitted to the ball, rotating it 90° to open or close the valve. The sealing principle of a ball valve seat varies with its structure; the seat designs in common use fall into two major categories: fixed seat with Floating ball, and floating seat with fixed ball.
When the seat is fixed and the ball floats, the ball is displaced in the direction of flow under fluid pressure, so that it contacts the seat downstream more tightly — that is, the specific pressure on that sealing surface increases, forming a single-side seal, while the specific pressure on the upstream seat sealing surface decreases accordingly and often cannot ensure sealing. When the seat floats and the ball is fixed, fluid pressure cannot displace the ball; instead the seat is pressed against the ball by a spring or by fluid thrust to establish the sealing specific pressure.
Structure
1. Soft-seated valve seats
(1) Conventional type
The conventional seat (Figure 1) is characterised in that, under pre-tightening force or fluid pressure, the seat is pressed tightly against the ball and the seat material undergoes elastic-plastic deformation to achieve sealing. Its sealing effect depends on the ability of the seat, under fluid pressure or pre-tightening force, to compensate for the roundness and microscopic surface irregularities of the ball. A sufficiently large sealing specific pressure must therefore exist between the seat and the ball.
(2) Elastic type
The elastic seat (Figure 2) uses elastic elements, such as metal spring frames and springs, which deform elastically under pre-tightening force or fluid pressure so as to compensate for the effect of changes in external conditions — temperature difference, pressure and wear — on the sealing performance of the ball.
(3) Spring-combination type
The spring-combination seat (Figure 3) relies on the thrust of a group of compression springs evenly distributed around the circumference of the valve passage cross-section, or of a single disc spring, so as to keep the seat pressed against the ball at all times and maintain the pre-tightened state.
(4) Piston type seat
The piston type seat (Figure 4) relies on the pressure of the inlet medium to generate the sealing force: the seat is pushed so as to press tightly against the ball, and the sealing ring undergoes elastic-plastic deformation to achieve sealing.
In a cut-off and relief seat, when the pressure inside the valve cavity rises abnormally above the downstream pressure, the resulting differential pressure produces an outward thrust that overcomes the spring force and moves the seat away from the ball, so that the cavity pressure is relieved downstream; afterwards, under the action of the spring, the seat comes back into contact with the ball.
In a double-movement seat, when the cavity pressure exceeds the outlet pressure, the seat is pressed tightly against the ball and the sealing ring undergoes elastic-plastic deformation to achieve sealing. In service, once the upstream seal fails unexpectedly and leakage occurs, the downstream seat provides the seal.
For double-stage sealing seats that are subjected to a relatively large sealing force, a combined rubber-and-plastic sealing structure is adopted: the rubber mainly performs the sealing function, while the plastic serves the dual purpose of support and auxiliary sealing.
(5) Special structure type
Special structure seats (Figure 5) include the internally or externally adjustable type, the bellows type, the grease-injection sealing type, the double-push type and the combination type.
In an internally adjustable seat, the sealing specific pressure between the seat and the ball is adjusted by an internal adjusting nut; its advantage is that there is no outward leakage point. In an externally adjustable seat, the sealing specific pressure between the seat and the ball is adjusted by an external adjusting screw plug, which presses a wedge to displace a telescopic sleeve.
A bellows-type seat is generally connected to the seat and the guide sleeve by electron beam welding or argon-arc welding. In design, the sealing centre of the seat should be kept smaller than the mean diameter of the bellows. This structure features reliable sealing, a large range of elastic compensation and flexibility in three-dimensional space.
A grease-injection sealing seat can improve sealing performance, reduce friction and wear of the seat, extend its service life, and prevent accidents caused by seat damage or fire during the service of the ball valve. A set of grease-injection holes may be added on the seat. Grease-injection sealing only acts as an auxiliary seal or as a temporary emergency measure.
In a double-push seat, when chamber N is connected to the control pressure, the seat is pressed tightly against the ball and maintains the seal. When the control pressure is applied to chamber M while chamber N is vented to atmosphere, the seat retracts and loses contact with the ball, so that wear and friction between the seat and the ball, as well as the operating torque, are smaller; this design is suitable for large-diameter ball valves at medium and high pressures. The combination type consists of a spring-group seat combined with a piston type seat. The former performs the main sealing function, while the latter is connected to the control pressure and provides auxiliary sealing.
2. Hard-seated valve seats
(1) Body overlay-welded type
In the body overlay-welded seat (Figure 6), a hard alloy is overlay-welded onto a metal material; the seat has an elastic tail seat, which helps to reduce friction damage to the sealing surface.
(2) Multilayer type
The multilayer sealing seat (Figure 7) is made by alternately stacking multiple layers of stainless steel sheet and thin graphite sheet and then rolling them under pressure by special processing, which improves its performance under high temperature and high pressure.
(3) Hollow tube type
In the hollow tube type sealing seat (Figure 8), bushings are fitted inside and outside, with a stainless steel tube in the middle; the elasticity of the hollow tube presses the seat tightly against the ball.
(4) Rotary type
The main feature of the rotary sealing seat (Figure 9) is that the seat can rotate about the axis of the passage while the valve is being opened and closed. In this design, a ring of teeth is distributed around the circumference of the seat, and each time the ball closes, the seat rotates by one tooth. In this way the seat wears uniformly around its circumference, which improves the working condition of the seat and extends its service life.
Sealing Materials
Seat sealing materials fall mainly into two categories: special polymers and metal seals.
1. Special polymer materials
Polymer materials are divided into two major classes: general-purpose polymers and special polymers. General-purpose polymers mainly include polyvinyl chloride, polyethylene, polypropylene, epoxy resin, phenolic resin and furan resin. Special polymers mainly include polytetrafluoroethylene, polychlorotrifluoroethylene, fluorinated ethylene propylene, polyether ether ketone and polyimide.
(1) Polytetrafluoroethylene
Polytetrafluoroethylene (PTFE-F4) has excellent heat resistance and cold resistance, together with non-stick properties, good self-lubrication and a low coefficient of friction (0.05), but it also has a tendency to cold flow. It can work continuously between -250 and 260 °C, can withstand a load of 5 MPa, and has a density of 2.2 g/cm3, a thermal conductivity of 0.25 W/(m·°C), a coefficient of linear expansion of (10–15) × 10-5/°C, a tensile strength of 10–30 MPa, an elastic modulus of 400 MPa, a compressive strength of 710 MPa and a flexural strength of 14 MPa. It resists media such as concentrated acids, concentrated alkalis, strong oxidising agents (such as aqua regia) and boiling hydrofluoric acid of any concentration.
(2) Polychlorotrifluoroethylene
Polychlorotrifluoroethylene (PCTFE-F3) has excellent cold resistance, high strength and hardness, good dimensional stability and no tendency to cold flow. Its service temperature is -195 to 120 °C; its density is 2.1 g/cm3, its thermal conductivity 0.058 W/(m·°C), its coefficient of linear expansion (415–710) × 10-5/°C, its tensile strength 35–40 MPa, its elastic modulus 1300 MPa, its compressive strength 50–70 MPa and its flexural strength 70 MPa. It resists inorganic acids at relatively high temperatures, and salt solutions and strong oxidising agents at relatively low temperatures, and it also resists most organic media at room temperature.
(3) Fluorinated ethylene propylene
Fluorinated ethylene propylene (PFEP-F46) offers high-temperature and low-temperature resistance and can work continuously in the range of -85 to 205 °C. Its density is 2.1 g/cm3, its thermal conductivity 0.25 W/(m·°C), its coefficient of linear expansion (9.5–19.6) × 10-5/°C, its tensile strength 19–20 MPa, its compressive strength 710 MPa and its flexural strength 14 MPa. Its chemical stability is comparable to that of polytetrafluoroethylene, and it resists inorganic acids, alkalis, alcohols, ketones, hydrocarbons, halogenated hydrocarbons, aromatic hydrocarbons, greases and detergents of various concentrations.
(4) Polyamide
Polyamide (N1010) has a relatively high tensile strength at room temperature, good impact toughness, high hardness and fatigue strength, and in particular excellent wear resistance and self-lubricating performance with a low coefficient of friction (0.03). Its density is 1.5 g/cm3, its thermal conductivity 0.25 W/(m·°C), its coefficient of linear expansion about 10.5 × 10⁻⁵/°C, its tensile strength 196 MPa, its elastic modulus 1300 MPa, its compressive strength 310 MPa and its flexural strength 310 MPa. It has good chemical resistance, resisting weak acids, weak alkalis and general solutions, and it has excellent oil resistance.
(5) Poly-p-phenylene
Poly-p-phenylene (PPL) features high-temperature resistance, resistance to chemical corrosion and to solvents, self-lubrication, radiation resistance and a low coefficient of friction (0.13). Its density is 2 g/cm3, its coefficient of linear expansion about 5.1 × 10⁻⁵/°C, its hardness 80 HS, its tensile strength 16 MPa, its compressive strength 48 MPa and its flexural strength 28 MPa. It resists corrosion by strong acids and alkalis such as sulfuric acid and hydrofluoric acid.
(6) Polyether ether ketone
Polyether ether ketone (PEEK) combines the heat resistance and chemical stability of thermosetting plastics with the moulding and processing performance of thermoplastics. Its continuous service temperature can reach above 240 °C, or above 300 °C when glass-fibre reinforced. Its density is 1.3 g/cm3, its tensile strength 162 MPa and its flexural strength 233 MPa. Apart from concentrated sulfuric acid and nitric acid, it resists attack by most organic and inorganic solvents, and it can be used continuously in steam at 200–260 °C.
(7) Polyimide
Polyimide (PI) is a new type of high-temperature-resistant engineering plastic that can be used continuously in air at -240 to 260 °C. It offers excellent electrical insulation, wear resistance, resistance to high-temperature radiation, and physical and mechanical properties. Its tensile strength is 100 MPa and its elastic modulus is 4 MPa. At room temperature it resists dilute acids and most organic solvents, but it is not resistant to strongly oxidising acids or strong acids, and it is not suitable for long-term immersion in water.
2. Metal sealing materials
Metal sealing surfaces have high hardness together with a suitable hardness difference. The hardness can be increased by surface hardening so as to enhance wear resistance. Metal sealing materials mainly include chromium-based hard alloys, cobalt-based hard alloys, nickel alloys, tungsten carbide and stainless steel (Table 1).
Table 1 Metal sealing materials
|
Material Code |
Service Conditions |
Hardness HRC |
|
Chromium-based cemented carbide |
||
|
D 507 |
For valves below 450°C |
≥ 40 |
|
D50Mo |
For valves below 510°C |
≥ 38 |
|
D54Mo |
For valves below 600°C |
≥ 37 |
|
D 577 |
For valves below 510°C |
≥ 28 |
|
Cobalt-based cemented carbide |
||
|
STL. 6 |
For valves below 650°C |
≥ 40 |
|
STL. 12 |
For valves below 650°C |
≥ 42 |
|
D 802 |
For valves below 650°C |
≥ 40 |
|
D 812 |
For valves below 650°C |
≥ 42 |
|
Nickel alloy |
||
|
Dni347 |
For sealing surfaces of nuclear power plant valves |
|
|
Dni357 |
For valve seat sealing surfaces in heat-resistant and corrosion-resistant media |
|
|
Tungsten carbide |
||
|
D 707 |
For valves below 650°C |
≥ 60 |
|
D 717 |
For valves below 650°C |
≥ 60 |
|
Stainless steel |
||
|
A 102 |
For corrosion-resistant valves below 300°C |
|
|
A 202 |
For non-oxidizing acids |
|
|
A 212 |
For urea and synthetic fiber media |
|
|
A 902 |
For sulfuric, nitric, and phosphoric acids and oxidizing acids, etc. |
|
Conclusion
The seat and the sealing ring are the key components of a ball valve. The sealing ring should have excellent stability, a relatively low coefficient of friction, resistance to ageing and good sealing performance. The seat should have a certain strength and rigidity, a moderate clearance, and should not deform easily under pressure. Metal-seated valve seats should meet the functions of high temperature, high pressure, severe corrosion, ultra-low temperature, zero leakage, long service life, fire safety, and resistance to pressure and wear.
Contact Person:Max.Song(SongShanshan)
Title:General Manager
Mobile:+86 15611322632
Tell:+86 10 89282693
Email:international@bvmc.com
Address:No. 3, Lvhai Road, Pangezhuang Town, Daxing District, Beijing


Copyright © Beijing Valve General Factory Co., Ltd.
SitemapThis website uses cookies to ensure you get the best experience on our website.


 Phone