Industrial Rising Stem Ball Valve
The industrial rising stem ball valve is a versatile and reliable fluid control device widely employed across diverse industrial sectors, valued for its robust performance, clear operational visibility, and long service life. Distinguished by its unique rising stem mechanism, this valve addresses key challenges in process management, making it a preferred choice for applications where safety and precision are paramount. At its core, the valve comprises several critical components: a durable body (typically forged or cast from carbon steel, stainless steel, or corrosion-resistant alloys to withstand high pressure and temperature), a spherical ball with a central bore, a rising stem connected to the ball, resilient seats that form a leak-tight seal between the ball and body, and an actuator (manual handle, gear operator, or automated system like pneumatic, hydraulic, or electric). The rising stem is the defining feature—when the valve opens, the stem extends upward from the body, and when closed, it retracts, providing an immediate visual indicator of the valve’s position to operators. The working principle is straightforward yet effective: a quarter-turn (90-degree rotation) of the actuator initiates movement. As the handle or actuator turns, the stem rises linearly and rotates the ball so its bore aligns with the pipeline, allowing unobstructed flow. Conversely, reversing the rotation lowers the stem, pressing the ball firmly against the seats to block flow and create a secure seal. This design minimizes friction between the stem and packing, reducing wear and extending the life of sealing components. Key advantages include: 1. Visual position confirmation: Eliminates guesswork about valve status, critical for safety in high-risk environments like oil refineries or chemical plants. 2. Reduced wear: The stem’s linear movement reduces contact with packing, lowering leakage risks and maintenance frequency. 3. Easy maintenance: Many models allow packing replacement without removing the valve from the pipeline, minimizing downtime. 4. High flow efficiency: Full-bore options ensure minimal pressure drop, ideal for large-volume flow applications. 5. Durability: Resistant to extreme conditions (high pressure, temperature, corrosive media) when constructed with appropriate materials. Common applications span oil and gas (upstream exploration, midstream transportation, downstream refining), chemical processing (handling aggressive chemicals), power generation (steam and water systems), water treatment plants, mining (slurry control), and pulp and paper manufacturing. In these sectors, the valve’s reliability and visibility make it indispensable for ensuring process safety and efficiency. To maintain optimal performance, regular maintenance is essential: inspecting packing for leaks, lubricating stem and actuator components, checking seat integrity for wear or damage, and verifying smooth stem movement. For automated valves, periodic checks of actuator functionality (e.g., air pressure for pneumatic systems, electrical connections for electric models) are necessary. In summary, the industrial rising stem ball valve combines functionality, durability, and safety, making it a cornerstone of fluid control in industrial operations worldwide. Its design ensures that processes run smoothly, securely, and with minimal interruptions.
Products
Category:
Ball Valve
-
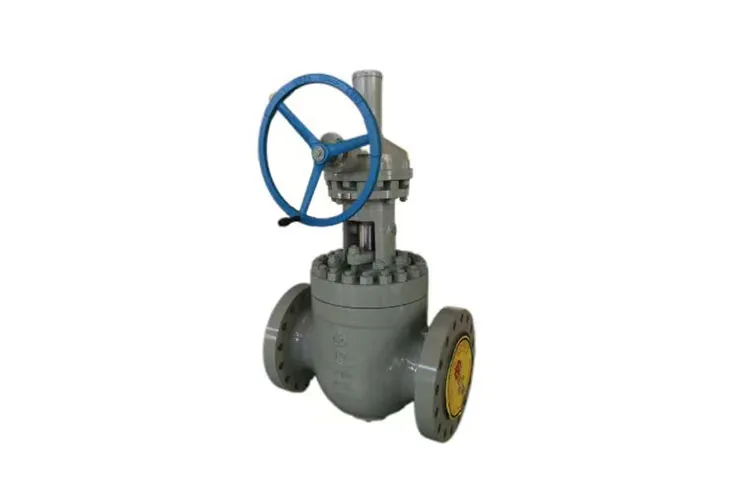
Industrial Pipeline Use Reliable Rising Stem Ball Valve
Category: Ball ValveBrowse number:Number:Release time: 2026-10-18 11:55:27The Industrial Pipeline Use Reliable Rising Stem Ball Valve is engineered for robust performance in demanding industrial and pipeline applications. Featuring a rising stem design, it provides clear visual indication of valve position, precise flow control, and enhanced safety. Constructed from high-quality corrosion-resistant materials, this ball valve delivers long-lasting durability, leak-free sealing, and reliable operation under high pressure and temperature conditions. Ideal for chemical, petrochemical, and oil & gas pipelines, it ensures efficient fluid regulation and system protection. Easy to maintain and install, this valve is a trusted solution for optimizing industrial flow control and pipeline safety.
News
Category:
-
[Industry News]Fixed Ball Valve Engineering Design Explained
2026-06-16 02:34:05
Case
Category:
No search results found!
Video
Category:
No search results found!
Download
Category:
No search results found!
Job
Category:
No search results found!
Featured Products
No search results found!


 Phone