Chemical Industry Nickel Alloy Forged Gate Valve
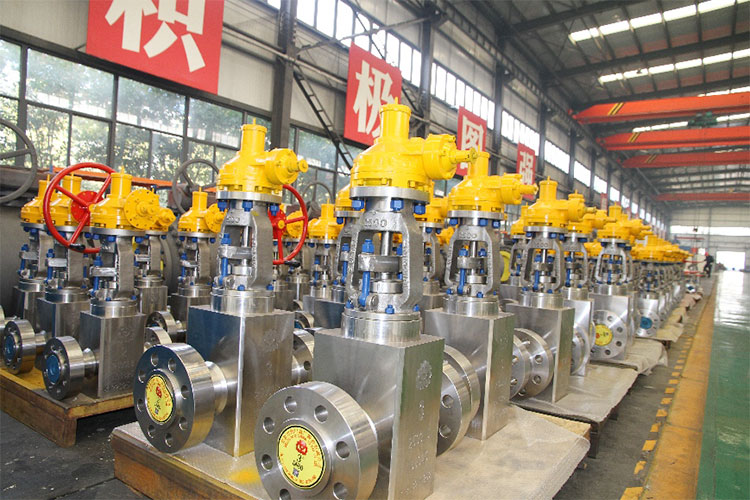
The Chemical Industry Nickel Alloy Forged Gate Valve is a critical fluid control component engineered to meet the harsh demands of chemical processing, where aggressive media, extreme temperatures, and high pressures are routine. Its robust construction and material selection make it an indispensable tool for ensuring operational safety, efficiency, and longevity across diverse chemical applications. At the heart of its performance lies the use of nickel alloys—such as Inconel, Hastelloy, or Monel—chosen for their exceptional corrosion resistance. These alloys excel in environments containing strong acids (sulfuric, hydrochloric, nitric), alkalis (caustic soda), chlorides, and organic solvents, which would quickly degrade standard steel valves. Additionally, nickel alloys retain mechanical strength at elevated temperatures (up to 1,200°F or higher) and resist oxidation, pitting, and stress corrosion cracking. The forged manufacturing process further enhances durability: forging eliminates porosity, creates a uniform dense grain structure, and boosts structural integrity compared to cast alternatives, enabling the valve to handle pressure ratings up to ANSI Class 2500 or beyond. Designed for reliability, the valve incorporates key safety and performance features. Its forged body and bonnet provide a leak-tight seal even under extreme pressure fluctuations. An anti-blowout stem prevents ejection during operation—a critical safeguard when handling hazardous chemicals. Metal-to-metal seating ensures a tight, long-lasting seal that performs consistently in high-temperature/pressure conditions, avoiding frequent soft seal replacements. Many models feature a full-port design, minimizing pressure drop and enabling easy pigging or cleaning—essential for maintaining product purity in pharmaceutical or food-grade chemical applications. The bolted bonnet design facilitates straightforward disassembly for maintenance, reducing downtime and operational costs. In the chemical industry, this valve is ubiquitous. It is a staple in petrochemical refineries for controlling crude oil, refined products, and process gases. In specialty chemical manufacturing, it handles corrosive intermediates and final products. Pharmaceutical plants rely on it for sterile fluid transfer, while agrochemical facilities use it to manage pesticide and fertilizer solutions. Offshore chemical platforms benefit from its saltwater corrosion resistance, making it suitable for subsea or coastal installations. Beyond material and design advantages, the valve offers unparalleled reliability. Its corrosion and wear resistance translate to longer service life, reducing replacement frequency and downtime. Low leakage rates prevent loss of valuable or hazardous materials, ensuring compliance with environmental regulations and workplace safety. Adherence to standards like API 600, ANSI B16.34, and ISO 9001 guarantees consistent performance and quality. Overall, the Chemical Industry Nickel Alloy Forged Gate Valve combines advanced materials with precision engineering to address the most challenging fluid control needs in the chemical sector. Its ability to withstand harsh conditions while maintaining reliability makes it a cornerstone of modern chemical processing operations.
Products
Category:
Severe Service Valve
-
Chemical Industry Nickel Alloy Forged Gate Valve
Category: Severe Service ValveBrowse number:Number:Release time: 2026-10-18 11:55:26The Chemical Industry Nickel Alloy Forged Gate Valve is designed for reliable isolation in highly corrosive and high-temperature chemical processing applications. Manufactured from premium forged nickel alloy materials, this gate valve offers exceptional resistance to corrosion, oxidation, and chemical attack, ensuring long service life and stable performance. Its forged body structure provides superior strength, tight sealing, and excellent pressure resistance under demanding operating conditions. Widely used in chemical plants, petrochemical systems, and specialty process pipelines, this valve meets strict industry standards and delivers safe, efficient, and low-maintenance flow control for critical chemical industry operations.
News
Category:
-
[Industry News]Fixed Ball Valve for Chemical Processing Plants
2026-05-31 06:33:20
Case
Category:
No search results found!
Video
Category:
No search results found!
Download
Category:
No search results found!
Job
Category:
No search results found!
Featured Products
No search results found!


 Phone