Chemical Grade DBB Valve
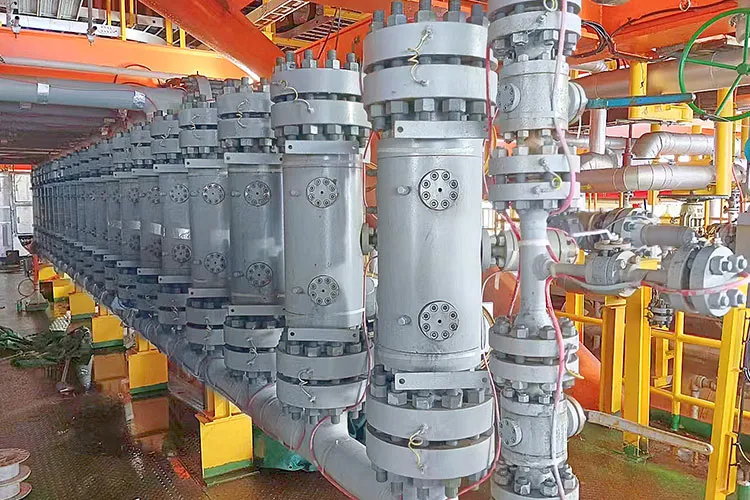
A chemical grade DBB (Double Block and Bleed) valve is a highly specialized isolation valve used primarily in demanding chemical processing applications. Designed to provide superior safety, reliability, and environmental protection, these valves play a crucial role in ensuring the integrity of fluid handling systems.The double block and bleed configuration consists of two isolation valves and a bleed valve within a single, compact body. This design permits the operator to securely isolate pipeline sections for maintenance, sampling, or instrument calibration without impacting system operation. By closing both block valves and opening the bleed valve, any trapped fluid between the seals can be drained or vented, allowing for immediate detection of leakage past the primary seal. This essential safety feature minimizes the risk of process fluid escaping into the environment or creating hazardous conditions for personnel.Chemical grade DBB valves are specifically engineered to withstand the severe conditions common in the chemical industry. They are typically constructed from high-grade materials such as stainless steel, Hastelloy, or other special alloys, ensuring corrosion resistance when exposed to aggressive media like acids, alkalis, solvents, and other toxic substances. Sealing elements are usually made from advanced elastomers or fluoropolymer materials compatible with a broad range of chemicals and resistant to temperature extremes.In terms of performance, these valves deliver zero leakage capability, tight shutoff, and low maintenance requirements. Their robust construction makes them suitable for both high- and low-pressure environments, while advanced seat and stem designs help to reduce fugitive emissions, meeting stringent environmental regulations. Most chemical grade DBB valves are offered in a variety of end connections—flanged, threaded, or welded—facilitating easy integration into new or existing pipeline systems.Operation can be manual or automated, providing flexibility for process control or emergency shutdown systems. Instrumentation interfaces are often incorporated, making the DBB valve ideal for safeguarding critical measurement devices or analyzers from process fluid during calibration or maintenance.In summary, chemical grade DBB valves are vital safety and isolation components, tailored for the rigorous demands of the chemical processing industry. Their double isolation, bleeder functionality, and robust construction significantly enhance safety, maintenance efficiency, and environmental stewardship within complex chemical installations.
Products
Category:
DBB Valve
-
Chemical Grade DBB Valve
Category: DBB ValveBrowse number:Number:Release time: 2026-10-18 11:55:26The Chemical Grade DBB (Double Block and Bleed) Valve is engineered for safe and reliable flow isolation in critical chemical processing applications. Designed to meet stringent industry standards, this valve provides dual sealing with a bleed function, ensuring complete system isolation and enhanced operational safety. Constructed from high-quality, corrosion-resistant materials, it offers exceptional durability, leak-tight performance, and long service life in harsh chemical environments. Ideal for pipelines handling acids, alkalis, and other aggressive chemicals, the valve minimizes maintenance, prevents cross-contamination, and enables precise flow control. This DBB valve is essential for chemical plants, petrochemical systems, and industrial processes requiring high safety and efficiency.
News
Category:
-
[Industry News]Solid Wedge Butterfly Valve Structure and Main Components
2026-05-29 07:18:52 -
[Industry News]Double Offset Valve Installation Guide and Best Practices
2026-05-09 06:51:45 -
[Industry News]Trunnion Mounted Ball Valve Performance Under High Pressure
2026-03-04 07:52:06
Case
Category:
No search results found!
Video
Category:
No search results found!
Download
Category:
No search results found!
Job
Category:
No search results found!
Featured Products
No search results found!


 Phone