Chemical DBB Valve
A Chemical DBB (Double Block and Bleed) valve is a specialized type of valve system widely utilized in the chemical industry for safety, isolation, and maintenance purposes. The principal feature distinguishing DBB valves is their ability to provide a dual barrier between process fluids and the environment, significantly reducing the chances of leakage and cross-contamination. This makes them ideal for handling hazardous, toxic, or high-value chemical flows where absolute isolation is paramount.Structurally, a DBB valve integrates two isolation valves and a bleed valve into a single compact unit. Both isolation valves can be operated independently to create two barriers against the flow, and the bleed valve, positioned between them, serves to safely vent trapped fluid or pressure from the space separating the isolation points. This configuration allows operators to verify that both obtained seals are holding, effectively confirming zero leakage from upstream or downstream sides.There are various designs of Chemical DBB valves—such as ball, needle, or gate types—each offering distinct advantages based on application requirements. Ball-type DBB valves are popular for their tight shutoff, durability, and minimal pressure drop, making them suitable for high-pressure and high-temperature chemical processes. The materials selected for DBB valves are similarly critical; they must exhibit exceptional resistance to corrosive chemicals, high pressures, and temperature fluctuations. Common materials include stainless steel, duplex alloys, and specialized superalloys for extremely aggressive environments.In operation, Chemical DBB valves enhance plant safety and operational efficiency. During maintenance, they allow the section of process piping to be completely isolated and depressurized, enabling workers to perform tasks without risk of exposure. The bleed feature not only detects and controls leaks but also facilitates the removal of residual fluids or pressure for safe interventions.Moreover, DBB valves reduce the number of connections and potential leak points by combining multiple valve functions within one body. This compactness contributes to space savings, reduced instrumentation complexity, and lower installation and maintenance costs, all of which are highly valued in the chemical industry’s tightly regulated environments.To sum up, Chemical DBB valves play a vital role in ensuring safe, reliable, and efficient operation of chemical processing plants. Their unique design delivers enhanced isolation performance, minimizes risks, and supports stringent safety standards required in modern chemical industries.
Products
Category:
DBB Valve
-
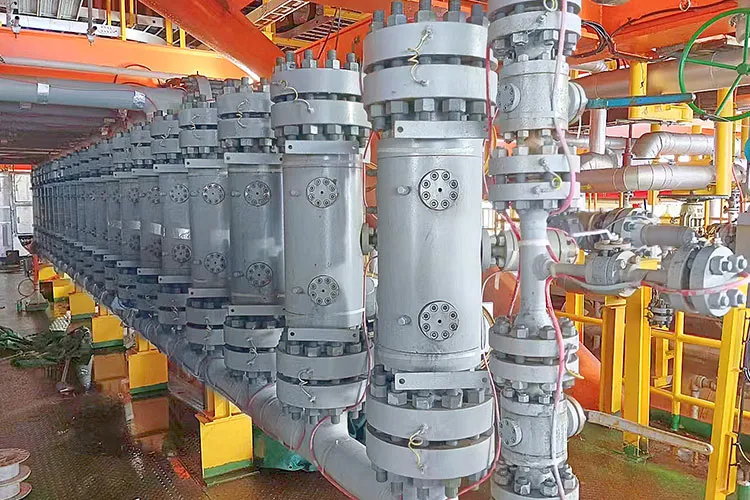
Chemical Grade DBB Valve
Category: DBB ValveBrowse number:Number:Release time: 2026-10-18 11:55:26The Chemical Grade DBB (Double Block and Bleed) Valve is engineered for safe and reliable flow isolation in critical chemical processing applications. Designed to meet stringent industry standards, this valve provides dual sealing with a bleed function, ensuring complete system isolation and enhanced operational safety. Constructed from high-quality, corrosion-resistant materials, it offers exceptional durability, leak-tight performance, and long service life in harsh chemical environments. Ideal for pipelines handling acids, alkalis, and other aggressive chemicals, the valve minimizes maintenance, prevents cross-contamination, and enables precise flow control. This DBB valve is essential for chemical plants, petrochemical systems, and industrial processes requiring high safety and efficiency.
News
Category:
-
[Industry News]Solid Wedge Butterfly Valve Structure and Main Components
2026-05-29 07:18:52
Case
Category:
No search results found!
Video
Category:
No search results found!
Download
Category:
No search results found!
Job
Category:
No search results found!
Featured Products
No search results found!


 Phone