Buried Pipeline Systems Industrial Underground Ball Valve
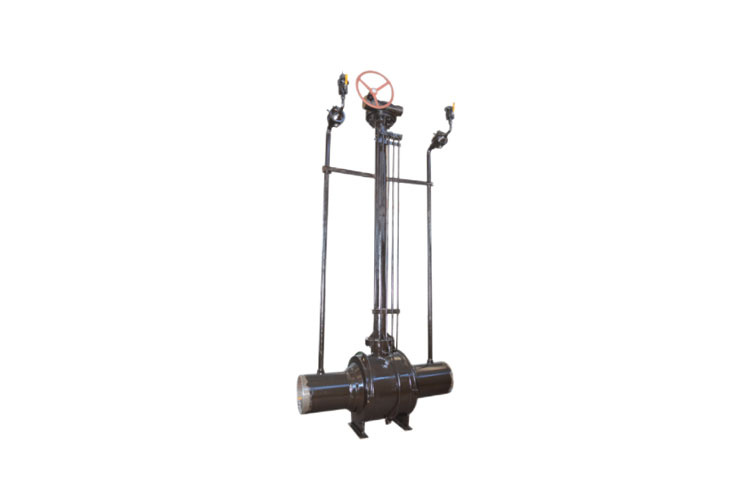
Buried pipeline systems form the invisible backbone of global industrial infrastructure, facilitating the transport of crude oil, natural gas, potable water, chemicals, and other critical fluids across vast distances. At the heart of these systems are industrial underground ball valves—specialized components designed to regulate, isolate, and control fluid flow with precision and durability in harsh subterranean environments. These valves are engineered to withstand extreme conditions that above-ground valves rarely encounter, making them indispensable for maintaining the integrity and efficiency of underground networks. Industrial underground ball valves are constructed with robust materials to resist corrosion, soil pressure, and temperature fluctuations. Common body materials include carbon steel, stainless steel, and high-alloy metals, selected based on the fluid type and environmental conditions. For example, valves handling corrosive chemicals may use Hastelloy or Inconel alloys, while those for water distribution might opt for coated carbon steel. The sealing elements—typically PTFE, EPDM, or nitrile rubber—ensure a tight, leak-proof seal even under high pressure, a critical feature given that underground leaks are costly to detect and repair. A defining feature of these valves is their extended stem design, which connects the ball mechanism to an above-ground actuator or handwheel. This allows operators to control the valve without excavating the buried line, simplifying operation and reducing maintenance downtime. Many models also feature full-bore construction, which minimizes flow resistance and allows for pigging (cleaning or inspection) of the pipeline without removing the valve. Performance-wise, underground ball valves excel in reliability. Their quarter-turn operation (90 degrees) enables quick shut-off, vital during emergencies to prevent spills or system failures. They are rated for a wide range of pressures (from low to high, up to 10,000 psi or more) and temperatures (-40°C to 300°C), making them suitable for diverse industrial applications. Anti-corrosion coatings, such as epoxy or fusion-bonded epoxy (FBE), further enhance their longevity by protecting against soil moisture and chemical attack. Installation requires careful consideration of soil conditions, pipeline alignment, and compatibility with existing systems. Flanged or welded connections are common, ensuring a secure fit that resists ground movement. Maintenance is minimal but essential: periodic inspection of the stem seal, actuator functionality, and pressure testing helps identify potential issues before they escalate. Replaceable components like seats and seals allow for repairs without full valve replacement, reducing operational costs. These valves find applications across multiple sectors. In oil and gas, they isolate pipeline sections for maintenance or emergency shut-off. Water utilities use them to regulate flow in distribution networks. Chemical plants rely on them for hazardous fluid transport, while mining operations deploy them for slurry and tailings pipelines. Compliance with international standards (e.g., API 6D, ISO 15848, ASME B16.34) ensures strict safety and performance criteria are met, protecting workers, the environment, and infrastructure. In conclusion, industrial underground ball valves are a cornerstone of reliable, safe, and efficient buried pipeline systems. Their robust design, corrosion resistance, and ease of operation make them essential for industries dependent on uninterrupted subterranean fluid transport.
Products
Category:
Ball Valve
-
Buried Pipeline Systems Industrial Underground Ball Valve
Category: Ball ValveBrowse number:Number:Release time: 2026-10-18 11:55:04The Buried Pipeline Systems Industrial Underground Ball Valve is engineered for durable, reliable performance in underground and buried pipeline applications. Designed to withstand harsh environmental conditions, this valve ensures secure flow control and isolation of liquids and gases in industrial pipelines. Its robust construction features corrosion-resistant materials, precise machining, and a rising or non-rising stem option, providing long-lasting operation and minimal maintenance. Ideal for oil, gas, water, and chemical distribution networks, this valve enhances pipeline safety, prevents leaks, and supports efficient system management. Trusted for performance and reliability, it is a key solution for buried pipeline infrastructure projects.
News
Category:
No search results found!
Case
Category:
No search results found!
Video
Category:
No search results found!
Download
Category:
No search results found!
Job
Category:
No search results found!
Featured Products
No search results found!


 Phone